en
 русский
 Español
 عربى

Membrane Helium Recovery Units for High-Purity Industrial Gas Recycling
Content
- 1 Introduction: Turning Helium Loss into a Reusable Industrial Resource
- 2 1. The Industrial Need for Helium Recovery
- 3 2. Product Overview
- 4 3. Membrane Separation Technology
- 5 4. Complete Process Flow
- 6 5. Main Advantages of the BHM Membrane Helium Recovery Unit
- 7 6. Comparison with Competing Technologies
- 8 7. Application-Specific Solutions
- 9 8. Manufacturing and Engineering Strengths
- 10 9. Automation, Monitoring, and Safety
- 11 10. Operation and Maintenance
- 12 11. Project Design and Selection Guidelines
- 13 12. Economic and Environmental Benefits
- 14 13. Quality and Reliability Considerations
- 15 14. Frequently Asked Questions
- 15.1 Q1: What is the main purpose of a membrane helium recovery unit?
- 15.2 Q2: How does the membrane separate helium from air?
- 15.3 Q3: Does the process require cryogenic temperatures?
- 15.4 Q4: Can the unit handle moisture and oil in the exhaust?
- 15.5 Q5: What helium purity can the system produce?
- 15.6 Q6: Is membrane separation better than PSA for every helium project?
- 15.7 Q7: Can the system operate continuously?
- 15.8 Q8: What happens if the product purity is temporarily below specification?
- 15.9 Q9: Is the unit suitable for leak-detection workshops?
- 15.10 Q10: What information is needed for equipment sizing?
- 15.11 Q11: How often do the membranes need to be replaced?
- 15.12 Q12: Can the equipment be expanded later?
- 16 15. Conclusion
- 17 References
- 18 Product: BHM Membrane Helium Recovery Unit
Introduction: Turning Helium Loss into a Reusable Industrial Resource
Helium is one of the most valuable industrial gases used in modern manufacturing, scientific research, medical technology, aerospace engineering, and precision testing. Its chemical inertness, low boiling point, thermal properties, and exceptional permeability make it indispensable in applications ranging from semiconductor processing and superconducting magnets to leak detection, optical-fiber manufacturing, welding, and aerospace testing. However, helium is also a non-renewable resource. Once released into the atmosphere, it is extremely difficult and economically impractical to recover naturally.
For many industrial users, helium consumption is not caused only by the gas required in the process itself. Large losses also occur when helium-rich tail gas is mixed with air, moisture, oil mist, dust, or other contaminants and then discharged. In conventional operations, this mixed exhaust is frequently treated as waste. The result is a low helium utilization rate, high dependence on purchased gas, exposure to supply-chain fluctuations, and increased operating costs.
The BHM Membrane Helium Recovery Unit is designed to address this problem through continuous recovery, purification, pressurization, storage, and reuse. Its core technology is ambient-temperature membrane separation. Instead of relying on cryogenic phase changes, chemical absorption, or adsorption regeneration, the system uses selective polymeric hollow-fiber membranes to separate helium from mixed process gas according to differences in permeability.
In a properly designed recovery system, helium-rich exhaust is collected at the point of use, stabilized in a buffer system, pretreated to remove harmful contaminants, separated through multiple membrane stages, analyzed online, compressed, and returned to the production process. Depending on the gas composition and the required outlet specification, the system can be configured to produce high-purity helium for industrial applications or ultra-high-purity helium for demanding semiconductor and scientific applications.
This article explains the working principle, process design, equipment configuration, application value, manufacturing capabilities, operational advantages, and selection considerations associated with the BHM Membrane Helium Recovery Unit.
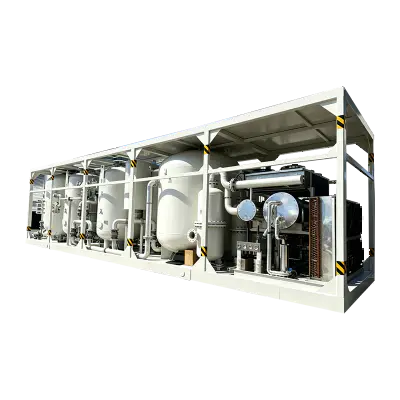
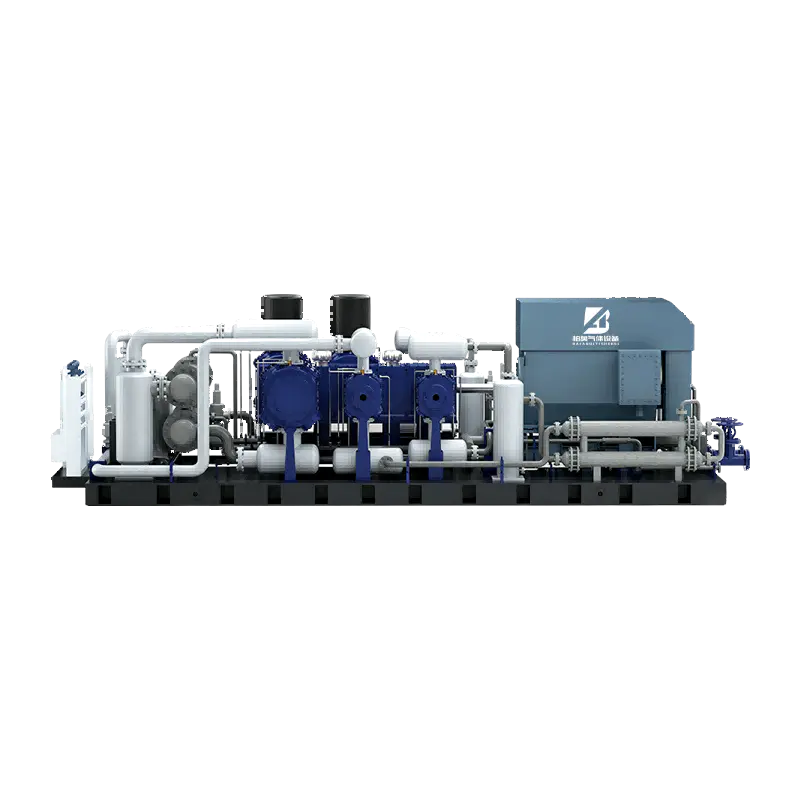
BHM Membrane Helium Recovery Unit
1. The Industrial Need for Helium Recovery
1.1 Helium Supply and Cost Challenges
Helium has a unique position in the industrial gas market. It cannot be manufactured economically through ordinary chemical synthesis, and commercial supplies are largely obtained from natural gas resources containing recoverable helium. Because production sources are geographically limited and global demand is distributed across many industries, helium prices can experience significant volatility.
Many users depend on cylinders, tube trailers, liquid helium deliveries, or centralized gas supply systems. These supply methods can be reliable under normal conditions, but they expose businesses to transportation costs, import dependence, delivery delays, contract limitations, and price changes. In high-consumption applications, even a small percentage of helium loss can generate substantial annual expenditure.
Direct venting is particularly wasteful in leak detection, where helium is deliberately introduced into a test component and later mixed with a large volume of air. Similar losses occur during equipment purging, maintenance, pressure release, superconducting magnet operation, optical-fiber production, and shielding-gas applications. Although the exhaust may contain a relatively low helium concentration, its total flow can represent a valuable recoverable resource.
1.2 The Consequences of Uncontrolled Discharge
Uncontrolled helium discharge creates several problems. The first is economic: purchased helium is consumed without generating additional production value. The second is operational: the plant becomes more dependent on external gas deliveries. The third is strategic: interruption of helium supply can affect critical manufacturing and research operations. The fourth is environmental and resource-related: a scarce natural resource is released instead of being circulated in a closed loop.
A helium recovery system does not eliminate the need for all fresh helium. Process requirements, unavoidable leakage, and gas-quality management still require makeup gas in many installations. However, a suitably designed recovery unit can significantly reduce fresh-gas demand. Depending on the application, gas composition, collection efficiency, and purification target, overall recovery can reach approximately 85 percent or higher, with selected high-purity applications designed for recovery in the 90 to 95 percent range.
2. Product Overview
2.1 Core Definition
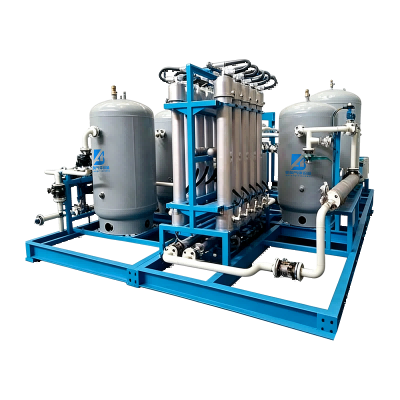
The BHM Membrane Helium Recovery Unit is an integrated gas recovery and purification system for collecting helium-containing exhaust and returning purified helium to industrial use. The unit combines gas collection, pressure stabilization, pretreatment, membrane separation, fine purification, online analysis, compression, storage, and automatic control.
The core separation step is a physical dissolution-diffusion process. Helium first dissolves into the selective membrane material, diffuses through the membrane structure, and exits on the low-pressure permeate side. Other gases with lower permeability are retained primarily on the feed or retentate side. The separation is driven by a difference in partial pressure rather than by a chemical reaction.
Because the process operates near ambient temperature, the unit does not require a cryogenic distillation column for its main separation function. It also avoids the cyclic adsorption and regeneration steps used in many pressure swing adsorption systems. This produces a compact and responsive process with relatively low auxiliary energy consumption and straightforward operating logic.
2.2 Modular Configuration
The unit can be configured for intermittent or continuous exhaust streams. Small and fluctuating flows can be handled through buffer tanks, flexible collection arrangements, and modular membrane skids. Continuous production lines can use sealed pipelines and centralized collection headers. Membrane modules may be arranged in series for deeper purification or in parallel for greater flow capacity.
Two broad product configurations are possible. A two-stage membrane arrangement with appropriate pretreatment and polishing can be used for stable 5N helium production in leak detection, welding, and related industrial applications. A three-stage arrangement combined with deoxidation, drying, and trace-impurity treatment can be designed for 6N helium applications in semiconductor processing and advanced scientific research.
3. Membrane Separation Technology
3.1 Dissolution-Diffusion Mechanism
Membrane gas separation is based on the different rates at which gases dissolve into and diffuse through a selective membrane. When the mixed gas contacts the membrane surface under pressure, each gas experiences a different transport behavior. Helium has a very small kinetic diameter and a high permeability through suitable polymeric materials. As a result, it can move through the membrane more rapidly than many of the gases present in the exhaust stream.
The membrane does not function like a conventional mechanical sieve with visible holes sized exactly to one molecule. Instead, molecular transport results from the interaction between gas solubility, molecular mobility, membrane structure, pressure difference, temperature, and material selectivity. For this reason, the membrane material and operating conditions must be carefully matched to the composition and pressure of the feed gas.
In the BHM system, specialized polyimide hollow-fiber membrane elements are used as the principal selective medium. Hollow-fiber construction provides a large membrane area within a compact module. This supports a high permeation flux while keeping the equipment footprint smaller than many conventional separation arrangements.
3.2 Relative Permeation Behavior
For the intended recovery conditions, the general permeation trend is described as:
Helium > Hydrogen > Oxygen > Nitrogen > Water Vapor > Oil and Other Heavy Impurities.
This ranking is a design basis rather than a universal value for every membrane material and process condition. Actual selectivity depends on membrane chemistry, pressure, temperature, feed concentration, humidity, contaminant loading, and module design. Nevertheless, the strong permeability of helium provides the foundation for recovering helium from air-containing tail gas.
Helium preferentially passes through the membrane and becomes enriched on the permeate side. Nitrogen, oxygen, carbon dioxide, dust, oil aerosols, and other low-permeability contaminants are more strongly retained upstream. The retentate stream may be discharged, treated further, or returned to an earlier process stage depending on the overall mass balance and recovery target.
3.3 Why Pretreatment Is Essential
Although the membrane material is designed for industrial service, reliable long-term performance depends on proper pretreatment. Oil droplets, condensed water, dust, aerosols, and process residues can foul membrane surfaces, block flow passages, alter selective-layer performance, or accelerate aging. Pretreatment therefore protects the most valuable separation components and stabilizes product quality.
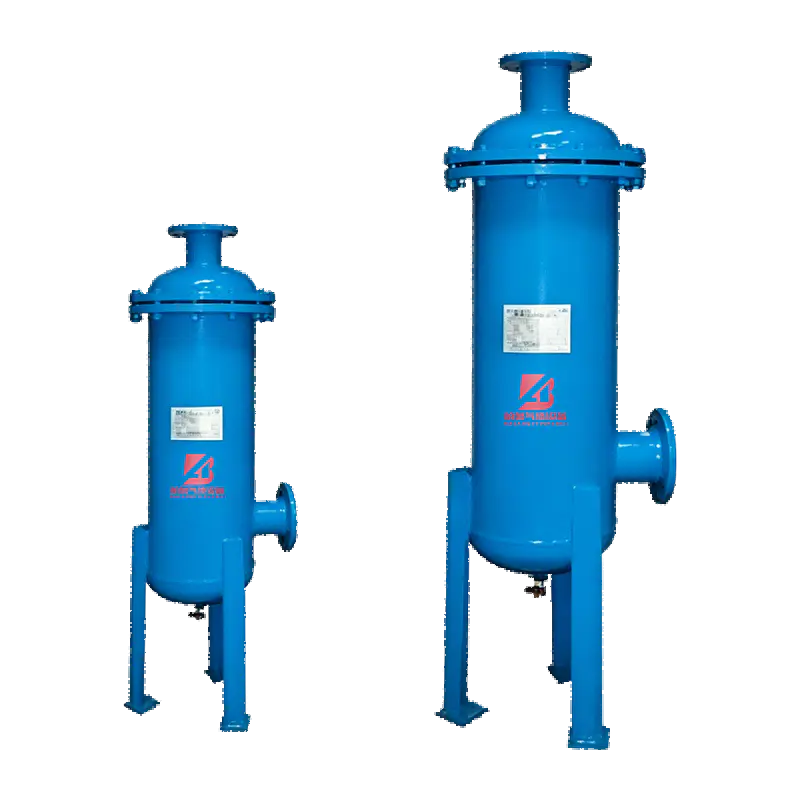
A typical pretreatment train includes a coarse particulate filter, a precision oil-removal filter, a water separator, and a drying unit. Where required, a refrigerated or cryogenic drying stage may be used to reduce moisture to a very low level. In demanding applications, the pretreatment system can be supplemented with activated-carbon protection, coalescing filtration, catalytic treatment, or application-specific impurity removal.
4. Complete Process Flow
4.1 Gas Collection
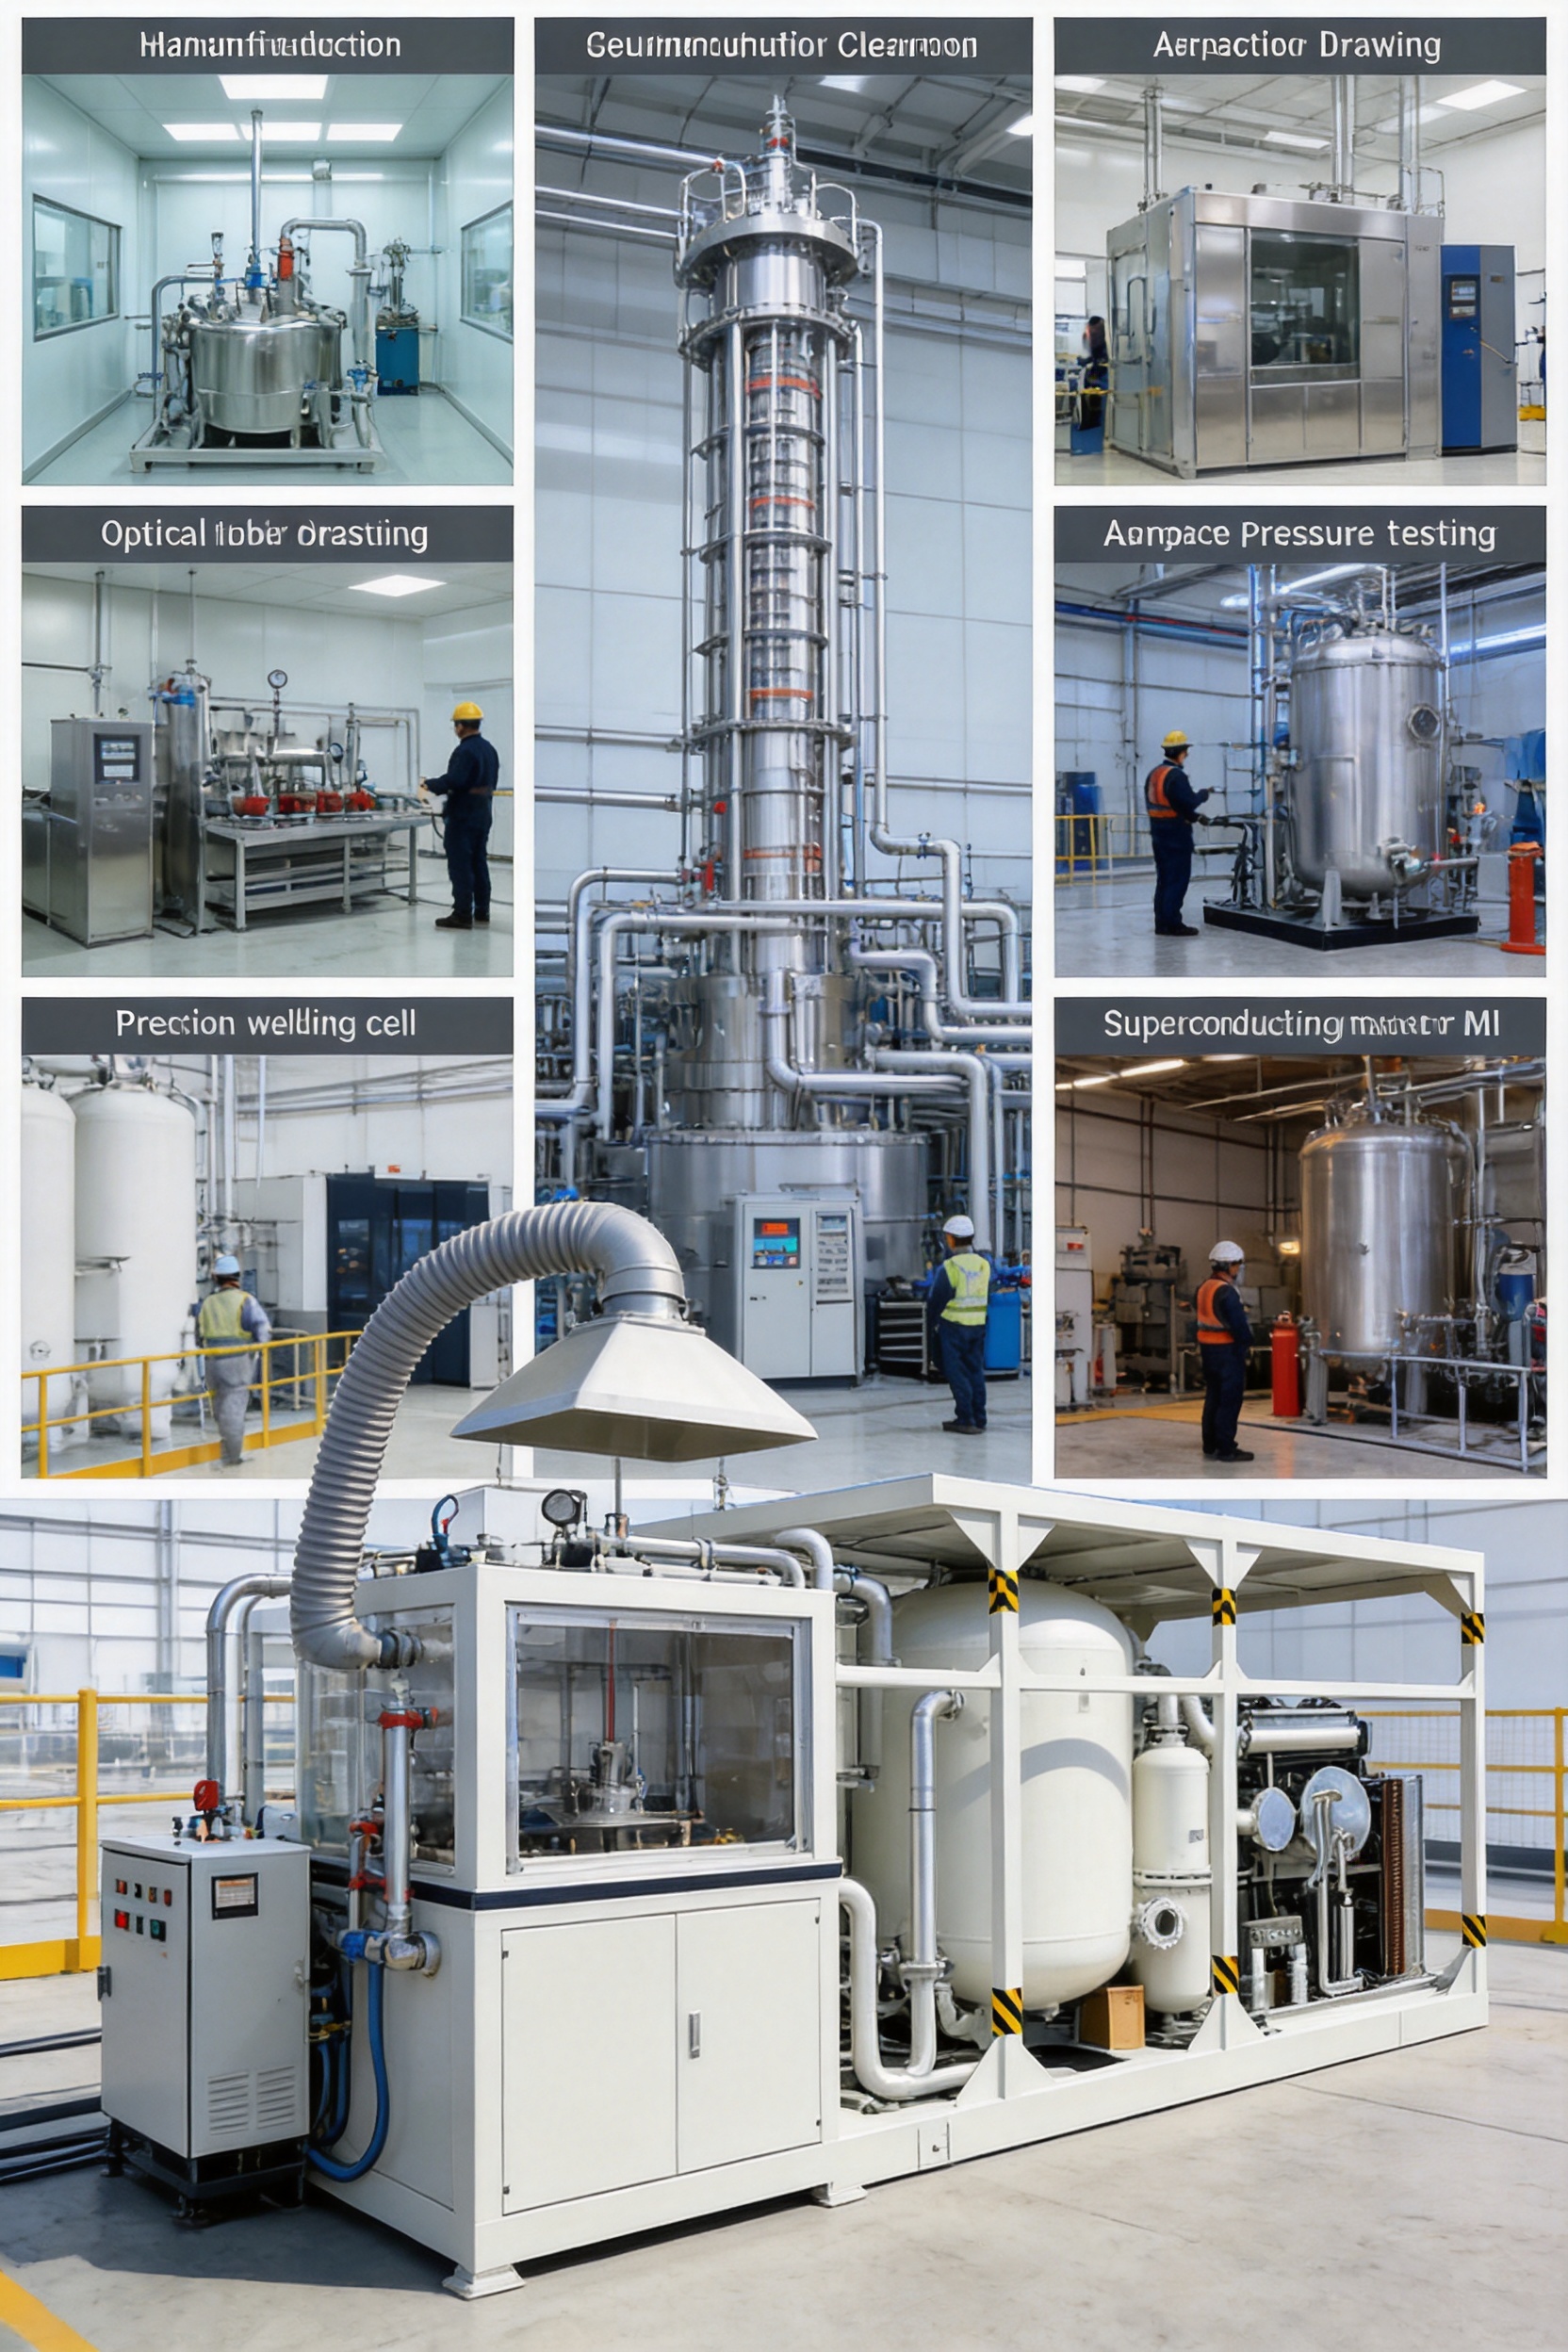
The recovery process begins with the collection of helium-containing exhaust. Collection design is often as important as membrane selection because helium is light, mobile, and easily lost through open or poorly sealed systems. Dedicated stainless-steel pipelines, sealed collection points, flexible hoods, and negative-pressure extraction arrangements can be used according to the operating scenario.
Continuous production applications such as semiconductor lines, optical-fiber facilities, and welding cells are well suited to closed pipeline collection. Intermittent applications such as leak testing, aerospace testing, and MRI maintenance may require flexible hoods, temporary connections, or buffer tanks. The objective is to capture the exhaust before it becomes excessively diluted or dispersed.
4.2 Pressure Stabilization and Buffering
Waste gas flow is rarely constant. A leak-testing workshop may release gas in short bursts, while an industrial production line may discharge continuously. Buffer tanks and pressure-control devices smooth these variations and provide a more stable feed to the pretreatment and membrane sections.
Pressure stabilization protects the membrane modules from sudden surges and helps maintain consistent separation performance. It also permits the recovery unit to continue operating when the upstream process temporarily stops. Automatic valves, pressure transmitters, flow meters, and safety relief devices are used to manage the gas path.
4.3 Coarse Filtration and Oil Removal
The first purification stage removes large particles and liquid droplets. Coalescing filters can capture oil aerosols and condensed moisture, while particulate filters protect downstream piping and modules from dust. Differential-pressure monitoring across the filters provides an indication of loading and helps operators schedule replacement before excessive pressure loss occurs.
For aerospace, automotive, and industrial leak-detection applications, the choice of filter media and drainage design is important because the exhaust may contain lubricants, test oils, or residues from the tested equipment. A well-designed filtration train prevents these contaminants from entering the membrane skid in harmful concentrations.
4.4 Drying and Moisture Control
Water vapor can affect membrane transport, condense in piping, and interfere with high-purity gas specifications. Drying equipment is therefore installed before the main membrane stages or between purification stages where required. The selection may include refrigerated dryers, adsorption dryers, cryogenic drying towers, membrane dryers, or combinations of these technologies.
The appropriate choice depends on the inlet moisture load, gas flow, ambient conditions, target dew point, and operating schedule. For semiconductor and scientific applications, trace moisture analyzers verify the final gas quality. In less demanding industrial applications, the drying system can be optimized for a balance between performance, capital cost, and energy consumption.
4.5 Primary Membrane Separation
After pretreatment, the gas enters the first membrane stage. This stage performs bulk helium enrichment and removes a significant portion of nitrogen, oxygen, and other slow-permeating components. The operating pressure, permeate pressure, membrane area, and stage-cut ratio are selected according to the inlet helium concentration and required recovery.
The first stage may produce an intermediate helium-rich stream rather than final product gas. This stream can be sent to a second membrane stage, a polishing unit, or a recycle loop. The retentate may contain residual helium, so the design should consider whether additional recovery is economically justified.
4.6 Secondary and Tertiary Purification
Secondary membrane separation increases helium concentration and reduces remaining impurities. Additional stages provide greater purification but may also reduce overall recovery if not balanced correctly. The process designer must therefore evaluate the relationship between purity, recovery, compression energy, membrane area, and reject-gas losses.
For 6N applications, membrane separation may be combined with catalytic deoxidation, final drying, trace impurity removal, and precision filtration. The membrane system performs the main enrichment duty, while polishing units address contaminants that require a different removal mechanism. This hybrid arrangement is more technically appropriate than expecting one separation technology to remove every impurity under every condition.
4.7 Detection, Compression, and Storage
Online analyzers measure helium purity and trace impurities such as oxygen and moisture. Gas chromatography can be used for composition analysis, while dedicated trace analyzers provide continuous monitoring of critical quality parameters. If product gas does not meet the preset specification, automatic control can divert it back to the purification section for additional treatment.
Qualified helium is then boosted to the required storage pressure. High-pressure gas tanks are appropriate for many industrial and semiconductor applications. Where the process requires liquid helium, a downstream liquefaction system and cryogenic storage tank may be incorporated. Liquefaction is therefore an optional final step for selected medical and scientific applications rather than the primary separation mechanism of the membrane unit.
5. Main Advantages of the BHM Membrane Helium Recovery Unit
5.1 Ambient-Temperature Operation
The system performs its principal separation function at or near ambient temperature. This avoids the extensive refrigeration and insulation infrastructure required by cryogenic distillation. It also reduces start-up complexity and makes the system easier to install near existing production equipment.
Ambient-temperature operation is particularly useful where gas is generated intermittently or where the user needs rapid response. The unit can be started and stopped more easily than a large cryogenic plant, while modular membrane sections can be isolated for inspection without shutting down the entire facility.
5.2 No Adsorbent Regeneration Cycle
Pressure swing adsorption systems depend on adsorbent beds and repeated adsorption, depressurization, purge, and regeneration cycles. Such systems can be highly effective for suitable gas separations, but they may involve valve switching, pressure fluctuations, adsorbent aging, dust generation, and periodic replacement.
The membrane recovery unit does not rely on cyclic adsorbent regeneration for its core separation. This simplifies the gas path and eliminates the need for frequent bed regeneration. Stable pressure-driven operation can also reduce purity fluctuations associated with switching sequences and adsorbent condition.
5.3 Lower Energy Demand Than Cryogenic Routes
Cryogenic distillation can produce very high-purity gases, but it requires substantial refrigeration, complex insulation, phase-change control, and careful management of low-temperature equipment. It is normally most attractive for very large gas volumes and suitable feed compositions.
For distributed industrial helium sources, membrane separation can provide a more practical balance of energy use, equipment size, and purification performance. The system still consumes energy for fans, pumps, compressors, dryers, analyzers, and controls, but the absence of a primary cryogenic separation stage can significantly reduce the overall auxiliary load.
5.4 Compact Modular Design
Hollow-fiber membrane modules provide a high separation area in a relatively compact volume. The complete recovery system can be assembled as a skid or modular equipment package. This is beneficial for factories with limited floor space, retrofit projects, and production lines that may require future expansion.
Parallel membrane modules increase capacity, while series modules improve purification depth. The modular approach also supports staged investment. A user may begin with one recovery train and add additional modules as helium consumption increases or as more exhaust sources are connected.
5.5 Fast Start-Up and Simple Operation
Membrane systems generally reach operating performance more quickly than large cryogenic plants. Once pressure, flow, temperature, and pretreatment conditions are established, the membrane modules can begin separating the gas without a long cool-down period.
Automatic control reduces the need for constant operator intervention. The PLC system can regulate feed pressure, collection pressure, valve position, flow, temperature, and product diversion. Alarm functions can identify high differential pressure, low purity, high moisture, abnormal compressor conditions, or leakage.
5.6 Adaptability to Mixed Industrial Exhaust
Many helium recovery applications do not provide a clean, constant, high-concentration feed. Leak-detection exhaust may contain air, water vapor, and oil. Aerospace exhaust may contain dust or traces of fuel residue. Welding and optical-fiber processes may produce continuous streams with changing impurity loads.
The BHM configuration addresses these conditions through graded pretreatment and staged purification. The membrane technology provides the central enrichment function, while filters, dryers, catalytic units, and fine purification equipment are selected according to the actual contaminant profile.
5.7 Reduced Fresh Helium Consumption
The main economic benefit is the reduction of purchased helium. A closed-loop system can return purified gas to the process, reducing cylinder, trailer, or liquid-helium deliveries. In applications with high annual consumption, the resulting savings can be substantial.
The exact savings depend on the initial helium concentration, collection efficiency, process leakage, required purity, operating hours, compressor efficiency, and reject-gas management. A detailed feasibility study should therefore be based on measured flow and composition rather than on a generic recovery percentage alone.
6. Comparison with Competing Technologies
| Evaluation Factor | Membrane Helium Recovery | Pressure Swing Adsorption | Cryogenic Distillation |
| Primary mechanism | Selective dissolution and diffusion through membranes | Pressure-dependent adsorption and regeneration | Low-temperature phase separation |
| Operating temperature | Near ambient | Usually near ambient | Very low temperature |
| Regeneration requirement | No core adsorbent regeneration | Required for adsorption beds | Not applicable, but refrigeration is required |
| Start-up behavior | Fast and suitable for intermittent operation | Moderate, with cyclic operation | Longer start-up and cool-down period |
| Equipment footprint | Compact and modular | Moderate, depending on bed size | Large and complex |
| Maintenance focus | Filters, analyzers, compressors, and membrane protection | Valves, adsorbents, switching controls, and filters | Refrigeration, insulation, columns, pumps, and controls |
| Best application range | Distributed and variable helium-containing exhaust | Suitable gas mixtures with compatible adsorption behavior | Large-scale, high-volume cryogenic gas processing |
| Expansion method | Add membrane modules in series or parallel | Add adsorption beds and associated controls | Major plant expansion |
This comparison does not mean that membrane separation is the correct solution for every gas separation project. Technology selection should be based on gas composition, flow rate, pressure, purity, recovery target, and economics. However, for many helium recovery projects involving distributed exhaust streams and variable flow, membrane separation offers a strong combination of flexibility, simplicity, and energy efficiency.
7. Application-Specific Solutions
7.1 Semiconductor Manufacturing
Semiconductor manufacturing requires extremely strict control of contamination. Helium may be used for equipment cooling, inert protection, process support, dust removal, and leak detection. The exhaust gas often has a relatively high helium concentration but may contain trace moisture, oxygen, particles, and organic compounds.
A semiconductor recovery system should use closed collection piping, high-efficiency particulate filtration, deep drying, multi-stage membrane separation, catalytic deoxidation, trace impurity polishing, and online analysis. Product gas that does not meet the required specification should be automatically diverted rather than sent directly to the process.
For advanced applications, a target of 99.9999 percent helium may be specified, with very low limits for oxygen and moisture. The recovery rate must be balanced against contamination control. In this scenario, protecting product quality is more important than maximizing recovery at the expense of impurity breakthrough.
7.2 MRI and Superconducting Systems
Medical superconducting magnets and scientific superconducting systems use helium for cryogenic cooling. Helium losses may result from vaporization, maintenance operations, pressure relief, and system servicing. The exhaust is often relatively clean, but collection must be carefully designed because helium can escape through small openings and ventilation systems.
A recovery arrangement can include sealed collection, pressure buffering, precision filtration, drying, membrane purification, compression, and re-liquefaction. The recovered gas may ultimately be stored as liquid helium for return to the magnet system. This configuration can reduce the frequency and volume of purchased liquid helium deliveries.
Medical installations require special attention to safety, reliability, noise, vibration, cleanliness, and fail-safe operation. The recovery unit should not interfere with magnet protection systems or emergency venting. Independent relief paths and automatic bypass arrangements are essential.
7.3 Industrial Leak Detection
Helium leak detection is one of the most attractive applications for recovery because the process often consumes a large volume of helium mixed with air. Tested components may include automotive parts, pressure vessels, vacuum equipment, valves, pipelines, battery systems, and precision assemblies.
The gas concentration can fluctuate considerably between test cycles. A flexible collection hood or sealed test-cell exhaust system can capture the mixed gas, while a buffer tank smooths the intermittent flow. Oil removal, water separation, multi-stage membrane enrichment, and final analysis are used to produce reusable 5N helium.
In a well-designed workshop, the recovery system can be connected to the leak detector supply line, creating a closed-loop arrangement. This reduces the amount of new helium needed for each test cycle and provides better control over gas costs as production volume increases.
7.4 Aerospace and Defense Testing
Aerospace applications may use helium for tank pressurization, pipeline purging, cryogenic testing, pneumatic systems, and specialized test procedures. These operations may involve high pressure, sudden discharge, large instantaneous flow, dust, and traces of fuel or process residue.
The recovery system must therefore include high-pressure buffer capacity, pressure-resistant piping, explosion-protection measures where required, suitable filtration, rapid pressure stabilization, and robust compressor controls. The membrane section should be protected from sudden pressure shocks and contaminants.
Because aerospace operations may be intermittent, the system should be able to enter standby mode without unnecessary gas loss. High-pressure storage allows recovered gas to be accumulated between test events and returned to service when the next operation begins.
7.5 Optical-Fiber Manufacturing
Helium is used as a carrier gas in optical-fiber preform production and related high-temperature processes. The gas may also support heat transfer and process stability. Because production can operate continuously, even a modest hourly loss can become a major annual consumption figure.
A sealed collection pipeline, stable-flow pretreatment system, multi-stage membrane separation unit, and pressure-controlled return line are appropriate for this application. The system should be designed for continuous operation and integrated with the factory’s process control architecture.
7.6 Precision Welding
Helium is used as a shielding gas in the welding of high-end alloys and components where oxidation control, arc characteristics, and heat transfer are important. Exhaust gas may contain air, moisture, welding fumes, and particulate contamination.
Efficient fume extraction and filtration are required before the gas reaches the membrane modules. Depending on the welding process, the recovered gas may be returned to a dedicated supply system after purification or blended with fresh helium under controlled conditions.
8. Manufacturing and Engineering Strengths
8.1 Integrated Product Development
The manufacturer behind the BHM product integrates research and development, process design, fabrication, installation, commissioning, and after-sales support. This integrated structure is valuable for helium recovery because the project is not limited to selecting a standard membrane skid. It also involves collection engineering, impurity analysis, pressure management, compressor matching, storage, control logic, and plant integration.
A single engineering organization can coordinate these elements from the initial feasibility study through final commissioning. This reduces the risk of mismatched equipment and enables the system to be adapted to actual operating conditions rather than relying only on a generic catalog configuration.
8.2 Experience in Gas Separation and Purification
The company has experience in gas-generation and purification equipment, including PSA nitrogen generators, PSA oxygen generators, membrane gas generators, nitrogen purification units, and hydrogen purification systems associated with ammonia decomposition. This broader gas-engineering background supports the design of complete gas treatment systems rather than isolated membrane components.
Experience across different separation technologies also helps engineers choose the most suitable combination of membrane separation, drying, filtration, catalytic treatment, compression, and storage. In applications where membrane separation alone cannot meet the final specification, the system can be supplemented with appropriate polishing technologies.
8.3 Standardized Manufacturing Facilities
The manufacturer operates a standardized workshop, office facilities, and warehouse resources that support equipment fabrication, assembly, inspection, and delivery. A structured production environment helps control skid dimensions, piping quality, electrical installation, labeling, documentation, and component traceability.
Standardization is especially important for modular membrane equipment. Repeatable fabrication methods can improve consistency between projects while still allowing customization of membrane area, piping size, control philosophy, tank capacity, compressor configuration, and purity instrumentation.
8.4 Custom Engineering for Industrial Conditions
Industrial helium exhaust varies widely. The feed may be dry or humid, clean or oil-contaminated, continuous or intermittent, low pressure or high pressure, concentrated or highly diluted. A successful recovery project must address these differences during the design stage.
The engineering process should begin with a gas survey covering helium concentration, total flow, pressure, temperature, moisture, oil content, oxygen, nitrogen, particulate loading, operating hours, and discharge pattern. The manufacturer can then determine the required pretreatment, membrane area, number of stages, storage volume, compressor capacity, and analyzer range.
8.5 Quality Control and Testing
Quality control should cover pressure vessels, pipelines, membrane modules, filters, valves, electrical panels, compressors, analyzers, and control software. Typical factory testing may include pressure testing, leak testing, electrical insulation checks, instrument calibration verification, valve-function testing, and control-sequence simulation.
Before shipment, the complete skid should be inspected against approved drawings and technical specifications. At the customer site, commissioning can include gas tightness verification, instrument calibration, membrane performance testing, product purity validation, emergency shutdown testing, and operator training.
8.6 Installation and After-Sales Service
Installation quality affects both recovery rate and safety. Improper piping, insufficient drainage, incorrect valve orientation, poor electrical grounding, or inadequate ventilation can compromise the system. A manufacturer with installation and service capability can support the customer during mechanical completion, start-up, optimization, and routine maintenance.
After-sales service may include spare filter elements, analyzer calibration, compressor servicing, membrane performance assessment, control-system updates, troubleshooting, and expansion planning. Remote monitoring and data logging can further improve response time and help identify declining performance before it causes a production interruption.
9. Automation, Monitoring, and Safety
9.1 PLC-Based Control
The PLC control system coordinates gas collection, pressure stabilization, filtration, membrane operation, product diversion, compression, and storage. Operators can view pressure, temperature, flow, valve status, purity, moisture, oxygen, compressor condition, and alarm history through a local human-machine interface.
Automatic sequencing reduces manual errors and permits unattended operation during stable production. The system can also adjust operating parameters in response to feed-flow changes, storage pressure, product purity, or process demand.
9.2 Product Quality Protection
Purity protection is essential when recovered gas is returned to a sensitive process. Online analyzers can establish high and low quality limits. If oxygen, moisture, or another impurity rises above the permitted value, the control system can close the product valve and route the gas back to purification or to a safe reject path.
This arrangement prevents a temporary disturbance from contaminating the downstream process. It also allows the recovery unit to continue operating while the cause of the quality deviation is investigated.
9.3 Inert-Gas Safety
Helium is chemically inert and nonflammable, but it can displace oxygen in enclosed spaces. The installation should therefore include adequate ventilation, oxygen-deficiency monitoring, warning alarms, and clearly defined emergency procedures.
Pressurized gas systems require pressure relief devices, correctly rated piping, secure supports, and inspection of tanks and fittings. Static grounding, electrical protection, and explosion-proof equipment should be applied where the surrounding process contains flammable substances or aerospace fuel residues.
9.4 Emergency Bypass and Shutdown
An emergency venting or bypass loop allows the system to isolate a malfunctioning section without creating unsafe pressure conditions. Automatic shutdown may be triggered by overpressure, compressor overload, high temperature, loss of cooling, analyzer failure, severe filter blockage, or low oxygen concentration in the equipment area.
The recovery system should never compromise the safety functions of the host production process. Emergency venting, process isolation, and equipment protection must be coordinated during the engineering and commissioning stages.
10. Operation and Maintenance
10.1 Routine Inspection
Operators should inspect pipeline tightness, flange connections, valve positions, filter differential pressure, compressor vibration, storage pressure, membrane operating pressure, and analyzer readings. Abnormal trends should be investigated before they become equipment failures or product-quality problems.
Because helium molecules are small and highly mobile, even small leaks can affect recovery performance. Periodic leak testing of the collection system and product piping is therefore recommended. Connections near compressors, storage vessels, flexible hoses, and instrument takeoffs deserve particular attention.
10.2 Filter and Dryer Maintenance
Filter elements should be replaced according to differential pressure, contamination level, or a preventive maintenance schedule. Oil-removal filters must be monitored carefully because oil carryover can damage downstream membrane performance. Drains should be checked to prevent liquid accumulation.
Drying equipment requires inspection of operating pressure, temperature, regeneration or refrigeration performance, dew point, and drainage. The maintenance interval should be based on actual moisture loading rather than on calendar time alone.
10.3 Analyzer Calibration
Gas chromatographs, oxygen analyzers, moisture analyzers, pressure transmitters, and flow meters require regular calibration. A drifted analyzer can cause either unnecessary product rejection or the delivery of gas that does not meet specification.
Calibration records should be retained as part of the plant quality system. For semiconductor, medical, aerospace, and scientific applications, traceable calibration and documented data history may be required.
10.4 Membrane Performance Monitoring
Membrane performance can be evaluated through helium recovery, product purity, permeate flow, retentate composition, pressure difference, and stage-cut behavior. A gradual decline may indicate contamination, compaction, seal damage, unexpected feed changes, or insufficient pretreatment.
Trend monitoring helps distinguish between a membrane issue and a problem elsewhere in the system. For example, a sudden purity decline may result from a failed dryer, a damaged filter, an analyzer fault, or a change in feed concentration rather than from normal membrane aging.
11. Project Design and Selection Guidelines
Before selecting a helium recovery unit, the user should collect representative operating data. A minimum survey should include:
- Helium concentration range and average concentration.
- Total exhaust flow, peak flow, and minimum flow.
- Operating pressure and temperature.
- Moisture, oxygen, nitrogen, oil, dust, and other contaminants.
- Continuous or intermittent operating pattern.
- Required product purity and allowable impurity limits.
- Required recovery rate and acceptable reject loss.
- Available electrical power, floor space, ventilation, and cooling utilities.
- Required storage pressure or liquid-helium interface.
- Applicable safety, quality, and documentation standards.
The recovery rate should be defined carefully. A membrane system may have a high helium recovery within the membrane train but a lower total plant recovery if collection losses, purge losses, compressor blowdown, and product rejection are included. A complete mass balance should therefore cover the entire system boundary.
Similarly, purity should be specified by individual impurity limits rather than by helium percentage alone. A gas containing 99.9999 percent helium may still be unsuitable for a particular process if its oxygen or moisture concentration exceeds the process limit.
12. Economic and Environmental Benefits
12.1 Reduced Gas Procurement
The most direct benefit is lower fresh helium consumption. By recovering gas that would otherwise be vented, the facility can reduce cylinder exchanges, bulk deliveries, liquid-helium purchases, and emergency procurement. The financial effect is greatest in operations with high gas prices, high working hours, and large exhaust volumes.
12.2 Improved Supply Security
On-site recovery provides a buffer against supply interruptions and price volatility. It does not make a facility completely independent of external supply, but it reduces the amount of fresh gas required to maintain production. This is particularly valuable for semiconductor plants, hospitals, research institutions, and aerospace operations where a gas shortage can delay high-value activities.
12.3 Lower Resource Waste
Helium is a finite natural resource. Recycling it extends the useful value of each purchased quantity and reduces avoidable discharge. The environmental benefit also includes lower transportation demand and reduced energy associated with repeated production, purification, compression, and delivery of replacement gas.
12.4 Potential Payback
Project payback depends on helium price, annual consumption, recovery percentage, operating hours, equipment cost, and maintenance requirements. In high-consumption applications, a payback period of approximately one to three years may be achievable, although each project must be evaluated using measured data and a complete cost model.
The cost model should include capital equipment, installation, piping, electrical work, compressors, storage, analyzers, maintenance, filter replacement, energy consumption, and potential downtime. It should also assign value to supply security and avoided production interruptions where appropriate.
13. Quality and Reliability Considerations
A helium recovery project should be treated as a process system, not simply as a membrane purchase. The membrane module is important, but the reliability of the complete installation depends on collection efficiency, pretreatment, pressure control, analyzer integrity, compressor performance, storage design, and automation.
Material selection is also important. Stainless-steel seamless piping is commonly preferred for clean gas service because it provides corrosion resistance, low contamination risk, and good mechanical durability. Seals, valves, filters, and flexible connections should be selected for helium service and for the pressure, temperature, and chemical conditions of the application.
Redundancy may be justified for critical systems. Parallel filters, standby compressors, duplicate analyzers, bypass lines, or spare membrane capacity can allow maintenance without interrupting production. The appropriate level of redundancy depends on the cost of downtime and the criticality of the helium supply.
14. Frequently Asked Questions
Q1: What is the main purpose of a membrane helium recovery unit?
The main purpose is to recover helium from exhaust gas that would otherwise be vented, purify it to a specified quality, compress it, store it, and return it to the production process. The unit is intended to reduce fresh helium consumption and improve supply security.
Q2: How does the membrane separate helium from air?
The membrane uses differences in gas permeability. Helium dissolves into and diffuses through the selective polymer membrane more readily than nitrogen, oxygen, carbon dioxide, water, and many heavier contaminants. A pressure difference drives the separation.
Q3: Does the process require cryogenic temperatures?
The principal membrane separation process operates at or near ambient temperature. Cryogenic equipment may be added later if the recovered helium must be liquefied, but cryogenic distillation is not required for the main enrichment step.
Q4: Can the unit handle moisture and oil in the exhaust?
It can be designed for exhaust containing moisture and limited oil contamination, but pretreatment is essential. Coalescing filters, oil-removal filters, water separators, and drying systems protect the membrane modules and stabilize product quality.
Q5: What helium purity can the system produce?
The target depends on the feed composition and process configuration. A two-stage membrane system with suitable pretreatment can be designed for 5N helium in many industrial applications. A three-stage system with deoxidation, drying, and trace-impurity polishing can be configured for 6N applications.
Q6: Is membrane separation better than PSA for every helium project?
No single technology is best for every application. Membrane separation is particularly attractive for variable, distributed, or moderate-flow helium exhaust because it is compact, continuous, and does not require adsorbent regeneration. PSA may be appropriate for other gas compositions or duties, while cryogenic processing may be justified for very large-scale projects.
Q7: Can the system operate continuously?
Yes. The system is designed for continuous operation and can be equipped with automatic pressure control, online analysis, product diversion, and fault alarms. Modular components may be arranged to support maintenance and future capacity expansion.
Q8: What happens if the product purity is temporarily below specification?
The control system can automatically divert unqualified gas back to the purification section or to a designated reject line. This prevents off-specification helium from entering the production process.
Q9: Is the unit suitable for leak-detection workshops?
Yes. Leak detection is a major application because the exhaust often contains recoverable helium mixed with air, water vapor, and oil residues. Flexible collection, buffering, oil removal, membrane enrichment, and pressure-controlled reuse are commonly applied.
Q10: What information is needed for equipment sizing?
Important information includes helium concentration, total and peak flow, pressure, temperature, moisture, oil content, operating hours, required purity, target recovery rate, storage pressure, and the pattern of gas release. Representative measurements provide a more reliable design than estimates based only on installed equipment capacity.
Q11: How often do the membranes need to be replaced?
Membrane service life depends on feed cleanliness, pressure, temperature, contaminants, operating hours, and mechanical integrity. Strong pretreatment and stable operation extend membrane life. Routine monitoring can identify performance decline and support maintenance planning.
Q12: Can the equipment be expanded later?
Yes. The modular structure allows additional membrane modules, filters, compressor capacity, storage tanks, or parallel trains to be added when the plant’s helium demand grows. Expansion should be considered during the initial layout and control-system design.
15. Conclusion
The BHM Membrane Helium Recovery Unit provides a practical route for converting helium-containing exhaust into a reusable industrial gas stream. Its central advantage is the use of selective membrane separation at ambient temperature, supported by comprehensive collection, pretreatment, staged purification, online analysis, compression, storage, and automatic control.
Compared with traditional approaches, the system avoids the main complexity of cryogenic distillation and eliminates the cyclic adsorbent regeneration required by PSA-based processes. Its modular architecture, fast start-up, low auxiliary energy demand, and adaptability to variable exhaust make it suitable for industrial leak detection, semiconductor manufacturing, MRI and superconducting systems, aerospace testing, optical-fiber production, and precision welding.
The performance of any helium recovery project depends on correct system integration. Efficient collection, accurate gas analysis, adequate pretreatment, appropriate membrane staging, reliable instrumentation, and careful safety design are all essential. When these elements are engineered together, the recovery unit can reduce virgin helium procurement, improve supply stability, lower resource waste, and support long-term closed-loop production.
Supported by experience in gas separation and purification equipment, standardized manufacturing resources, customized engineering, installation capability, and after-sales service, the manufacturer is positioned to provide complete helium recovery solutions rather than isolated equipment modules. For facilities seeking to reduce helium costs and strengthen operational independence, a properly designed membrane recovery system offers a scalable and technically sound investment.
References
1. Baker, R. W. Membrane Technology and Applications. Fundamentals of gas transport, membrane materials, and industrial membrane system design.
2. American Society of Mechanical Engineers. Pressure Vessel and Piping Engineering Principles. General guidance for pressure-containing equipment, piping integrity, and safety design.
3. International Organization for Standardization. Gas Analysis and High-Purity Gas Handling Practices. General principles for sampling, analysis, calibration, and quality control.
4. International Organization for Standardization. Industrial Gas Safety and Management Guidance. Recommendations concerning storage, distribution, pressure control, and workplace safety.
5. Perry’s Chemical Engineers’ Handbook. Gas separation, process design, pressure drop, filtration, drying, compression, and industrial equipment selection.
6. Industrial membrane separation literature covering polymeric hollow-fiber membranes, dissolution-diffusion transport, gas permeability, selectivity, fouling control, and module engineering.
7. Technical literature on helium conservation in leak detection, semiconductor processing, superconducting magnet systems, aerospace testing, optical-fiber manufacturing, and precision welding.
Product: BHM Membrane Helium Recovery Unit
- Tel: +86-15057127179
+86-13588382771 - Email: huang.yifan0215@gmail.com
- Address: Huanshan Township, Fuyang District, Hangzhou City, Zhejiang Province
Copyright © Zhejiang Baiao Gas Equipment Co., Ltd. All Rights Reserved.
Privacy
Gas Generator Plant Manufacturer, Industrial Purification Equipment Plant